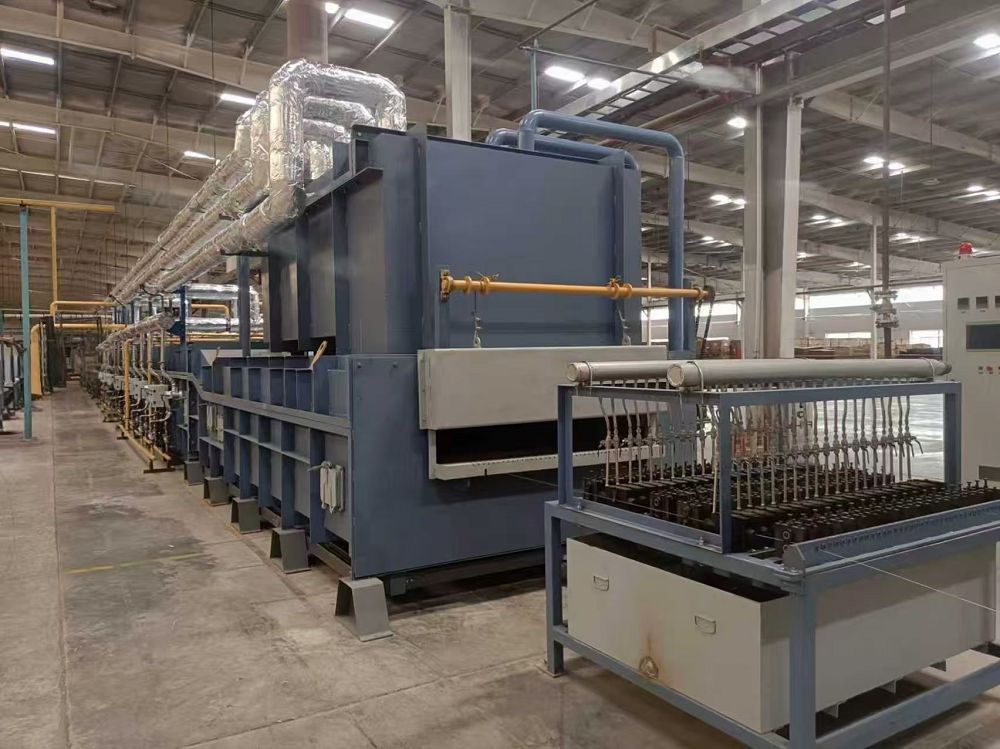
"Galvanize-then-draw" process: To enhance the properties of galvanized steel wire, a process involving lead patenting, galvanizing, and subsequent drawing to the finished size is employed. The typical workflow is: steel wire → lead patenting → galvanizing → drawing → finished steel wire. This is the method with the shortest process flow among galvanizing and drawing techniques; it can be applied following either hot-dip galvanizing or electro-galvanizing. Drawing after hot-dip galvanizing yields better mechanical properties than drawing before galvanizing, while drawing after electro-galvanizing results in a dense, durable zinc coating. Both methods produce a thin, uniform zinc coating, thereby reducing zinc consumption and the load on the galvanizing production line.
"Intermediate galvanizing-then-drawing" process: The workflow for this process is: steel wire → lead patenting → first drawing → galvanizing → second drawing → finished steel wire. Its defining characteristic is that the lead-patented wire undergoes an initial drawing stage, is galvanized, and then undergoes a second drawing stage to reach the finished size; since galvanizing occurs between the two drawing stages, it is termed "intermediate galvanizing." Wire produced via this method features a thicker zinc coating than that produced by the "galvanize-then-draw" method. When hot-dip galvanizing is used in this intermediate process, a high total reduction ratio (from lead patenting to the finished product) can be achieved, resulting in superior wire properties compared to the standard "galvanize-then-draw" method.
"Hybrid galvanizing-drawing" process: To produce ultra-high-strength (3000 N/mm²) galvanized steel wire, a "hybrid galvanizing-drawing" process is used. The typical workflow is as follows: lead patenting → first drawing → pre-galvanizing → second drawing → final galvanizing → third drawing (dry drawing) → wet drawing (water tank) → finished steel wire. This process enables the production of ultra-high-strength galvanized steel wire with a carbon content of 0.93–0.97%, a diameter of 0.26 mm, and a tensile strength of 3921 N/mm². During drawing, the zinc coating protects and lubricates the wire surface, and no wire breakage occurs.